Precision Components & OEM Guitars Tailored for Greek Importers
Designed for professional luthiers, regional instrument workshops in Athens and Thessaloniki, and retail distributors requiring strict dimensional tolerance, uncompromised resonance, and thermal-treated moisture stability.
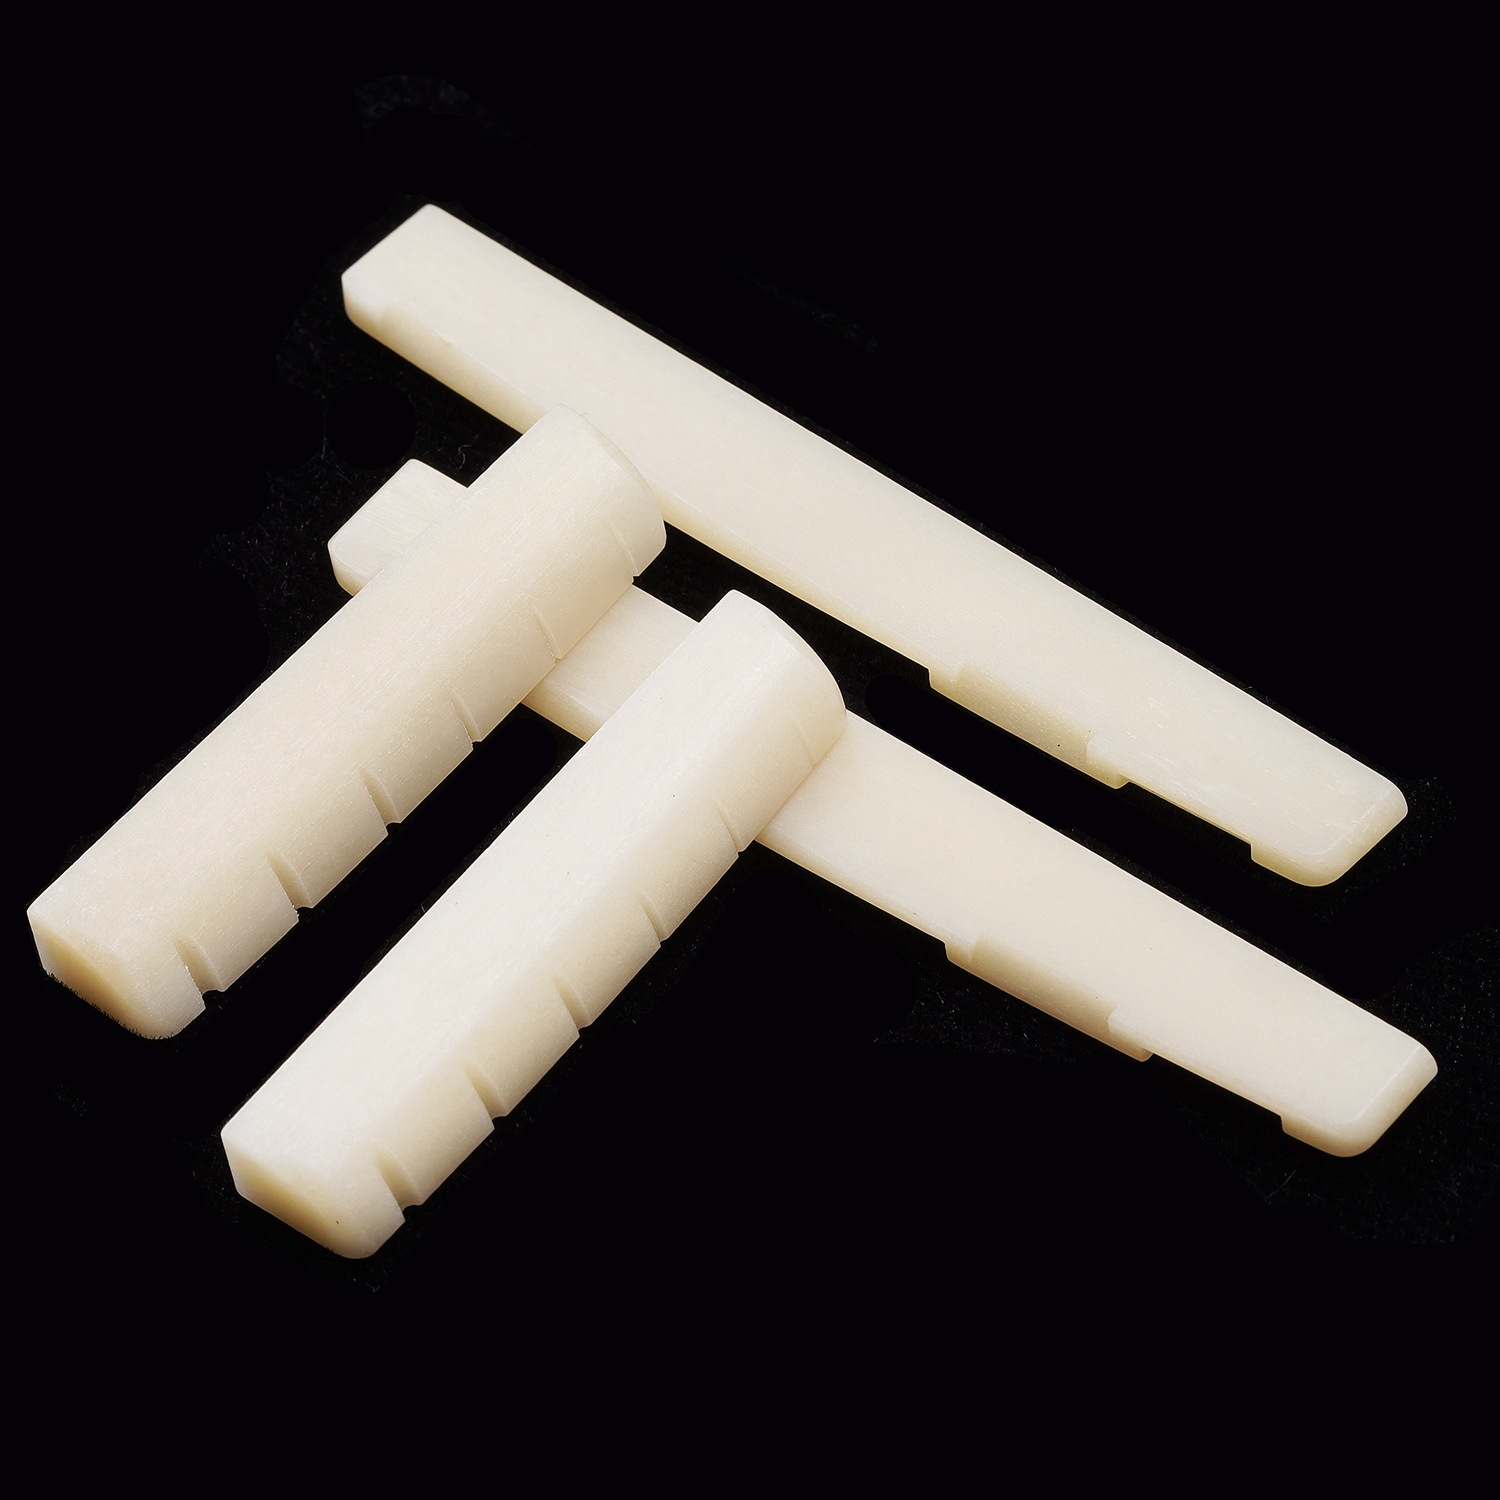
Acoustic Guitar Bone Nut Saddle Bridge Nut 43mm 74mm Natural Unbleached
- High-density unbleached natural bovine bone
- Zero sonic porosity for optimal string sustain
- Ideal for traditional folk & bouzouki conversion
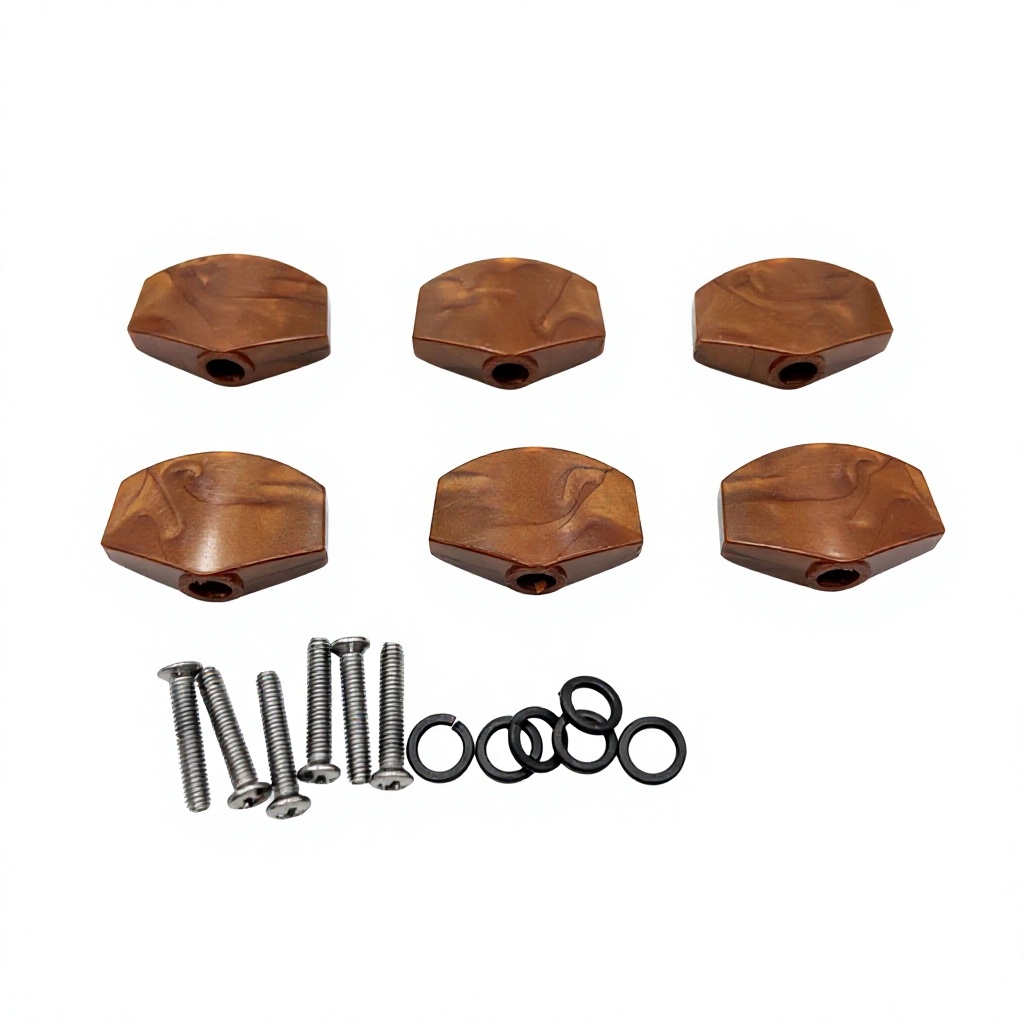
Plastic Guitar Tuning Knob Caps 6 Pieces Set for Acoustic Classical Guitar Handle Replacement
- Impact-resistant UV-stabilized polymer
- Universal spline fit for classical machine heads
- Resistant to Mediterranean salt air degradation
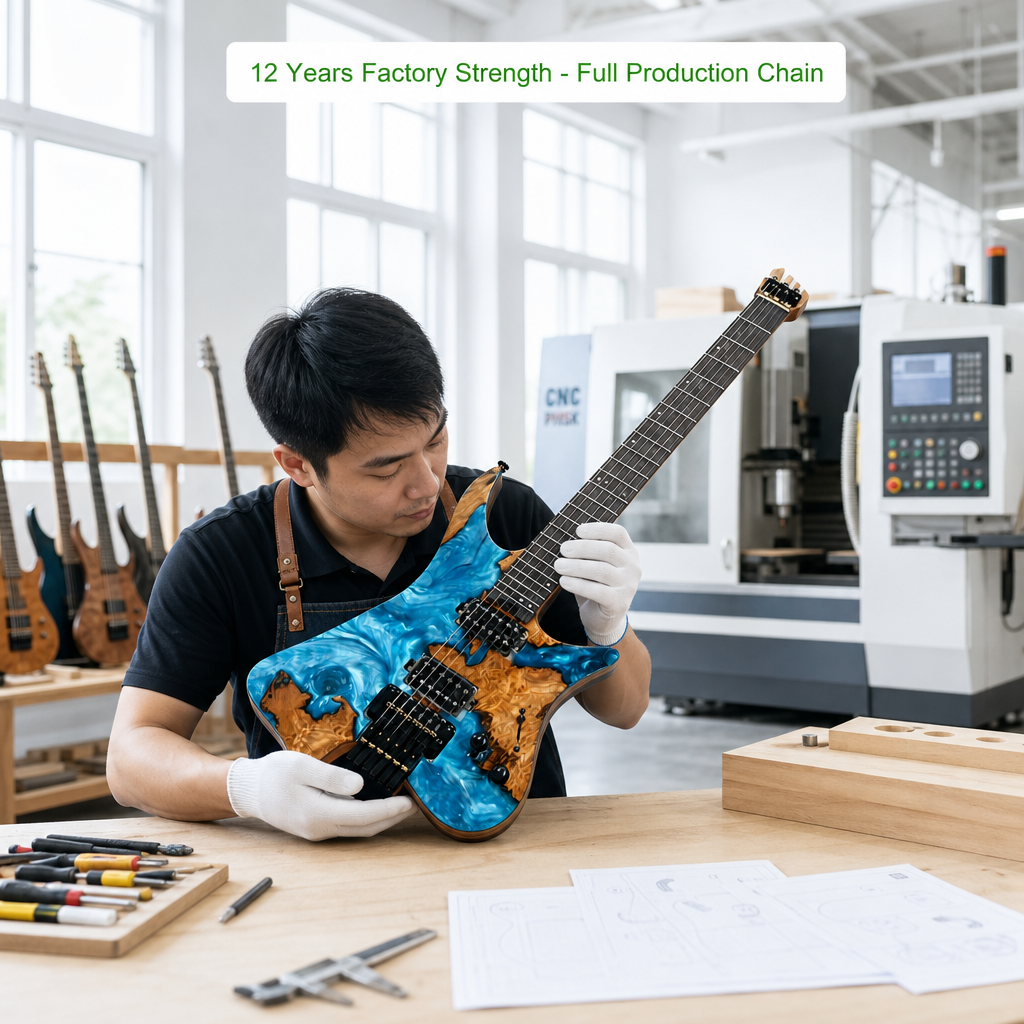
Headboard Electric Guitar With Bright Light High-quality Electric Guitar Factory OEM ODM Small Double-fret Bridge
- Precision engineered dual-action truss system
- Custom fingerboard bevel with illuminated accents
- CNC-dressed fret ends for rapid chromatic shifts
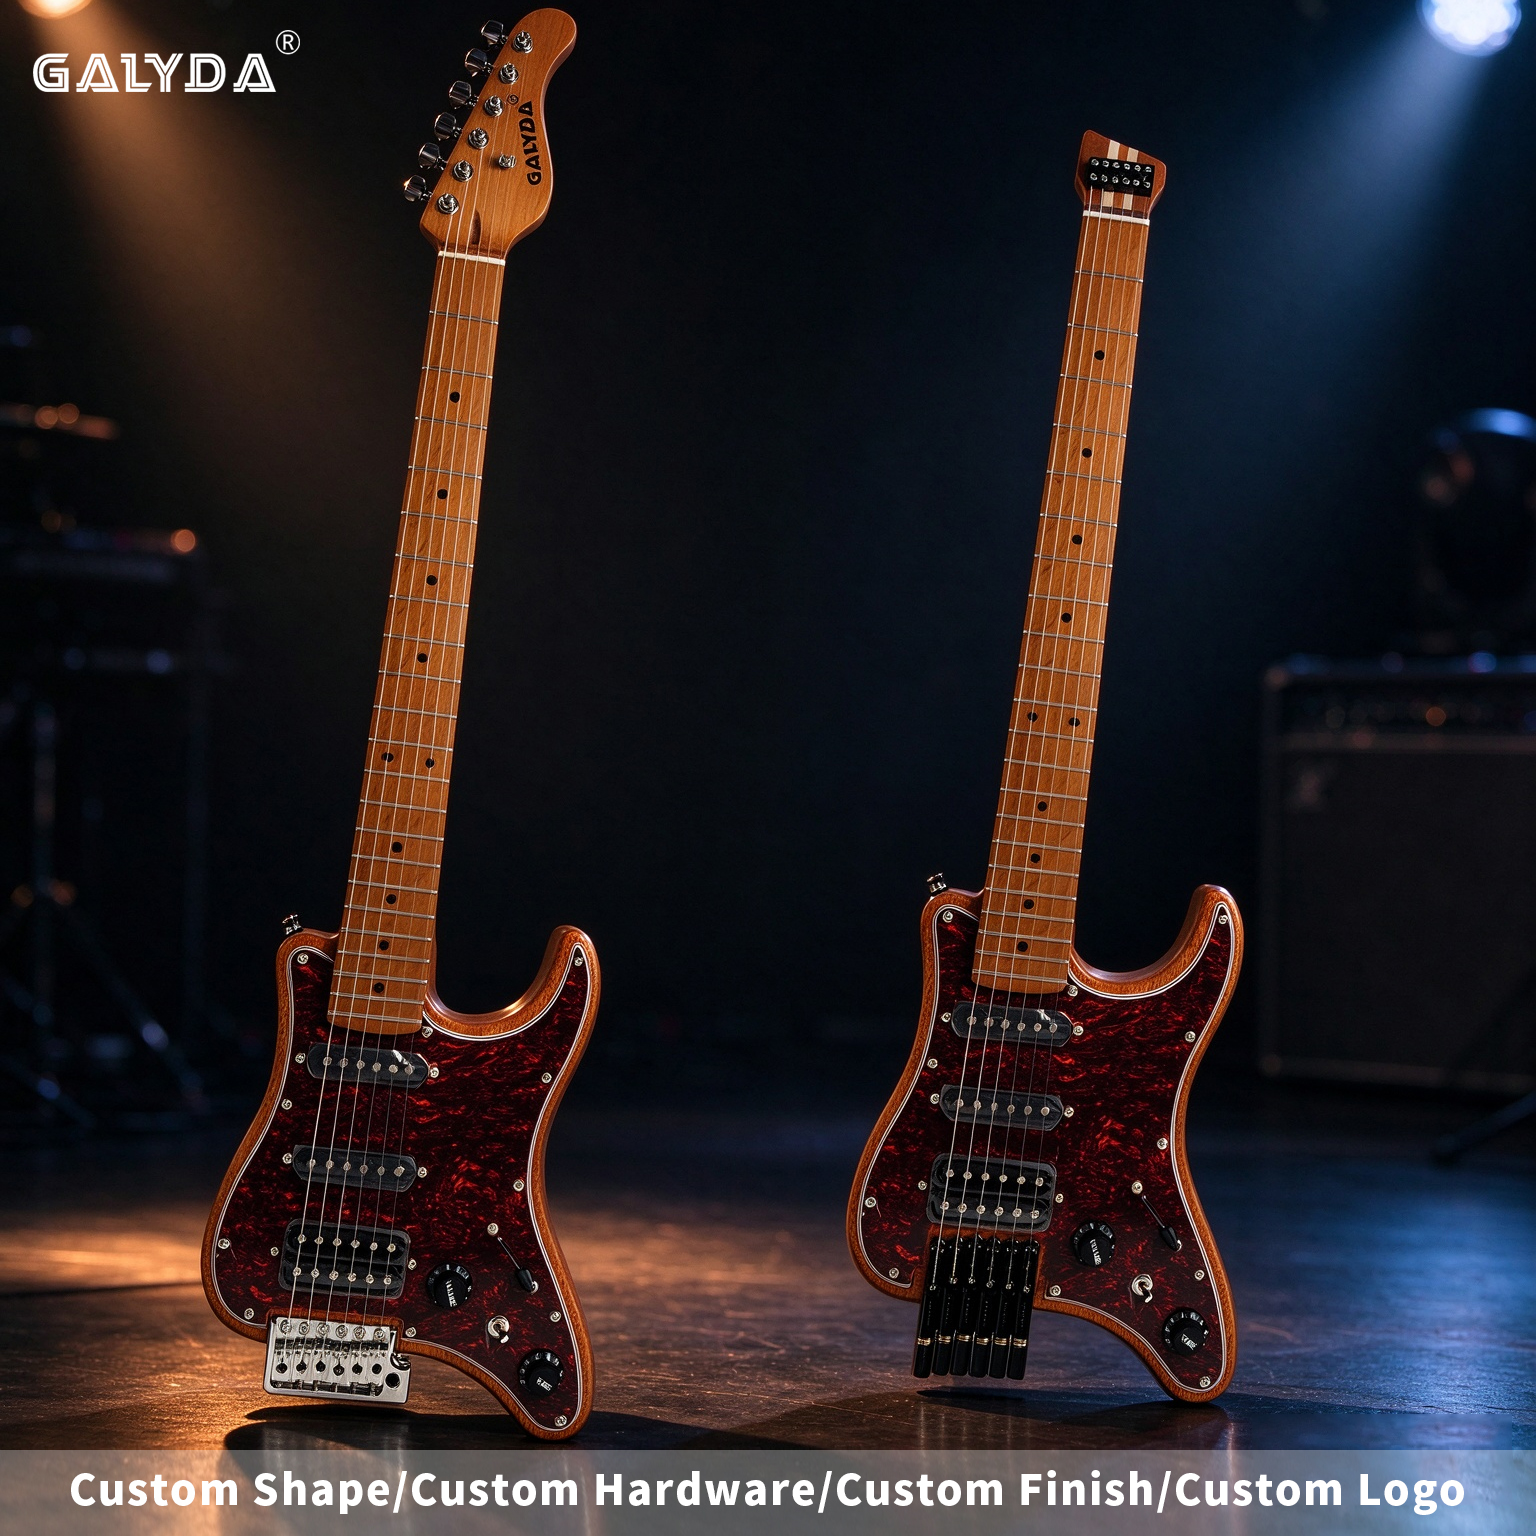
OEM ODM Electric Guitar SSH Pickups Unique Shape Custom Finish Custom Hardware Factory Custom
- Alnico V staggered magnets for dynamic clarity
- Hum-cancelling bridge coils with high headroom
- Wax potted against Aegean high-heat vibration
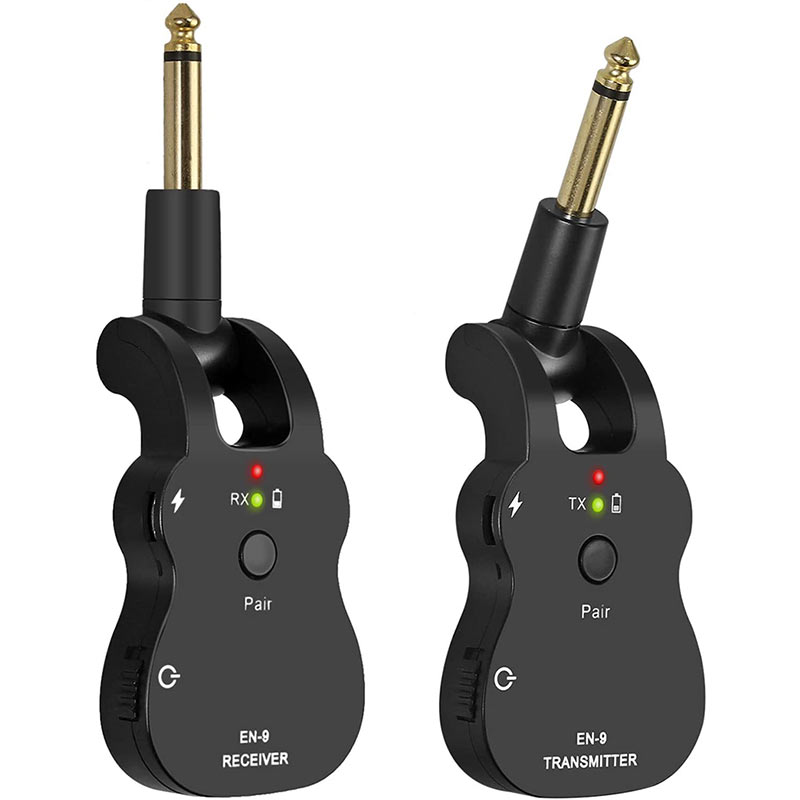
High Quality Wholesale Custom Cheap Digital Guitar Bass Audio Transmitter and Receiver Wireless Guitar Transmitter System
- 2.4GHz uncompressed low-latency (<5ms) design
- Tested over 30-meter open stage ranges
- CE & FCC certified for Greek EU compliance
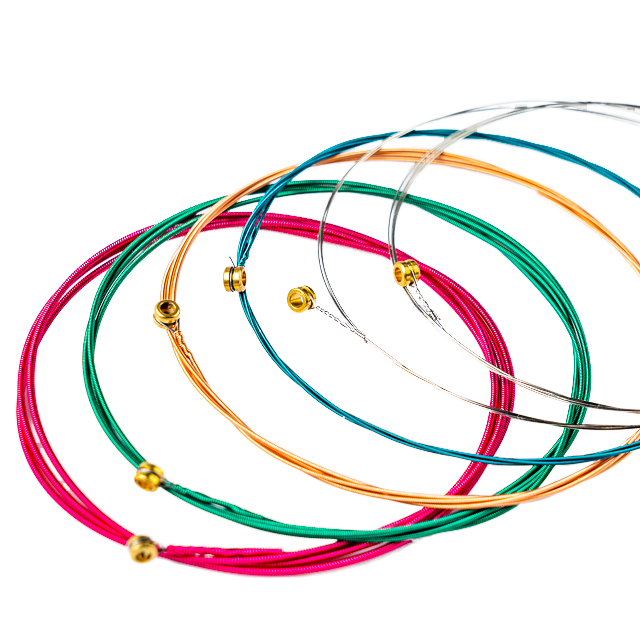
Set of Colorful 6-String Electric Guitar Acoustic Guitar Strings Steel Tone 1048 Series
- Anti-corrosion coated high-carbon hexagonal core
- Vibrant color-coding for music academies
- Sealed nitrogen foil packaging against maritime moisture
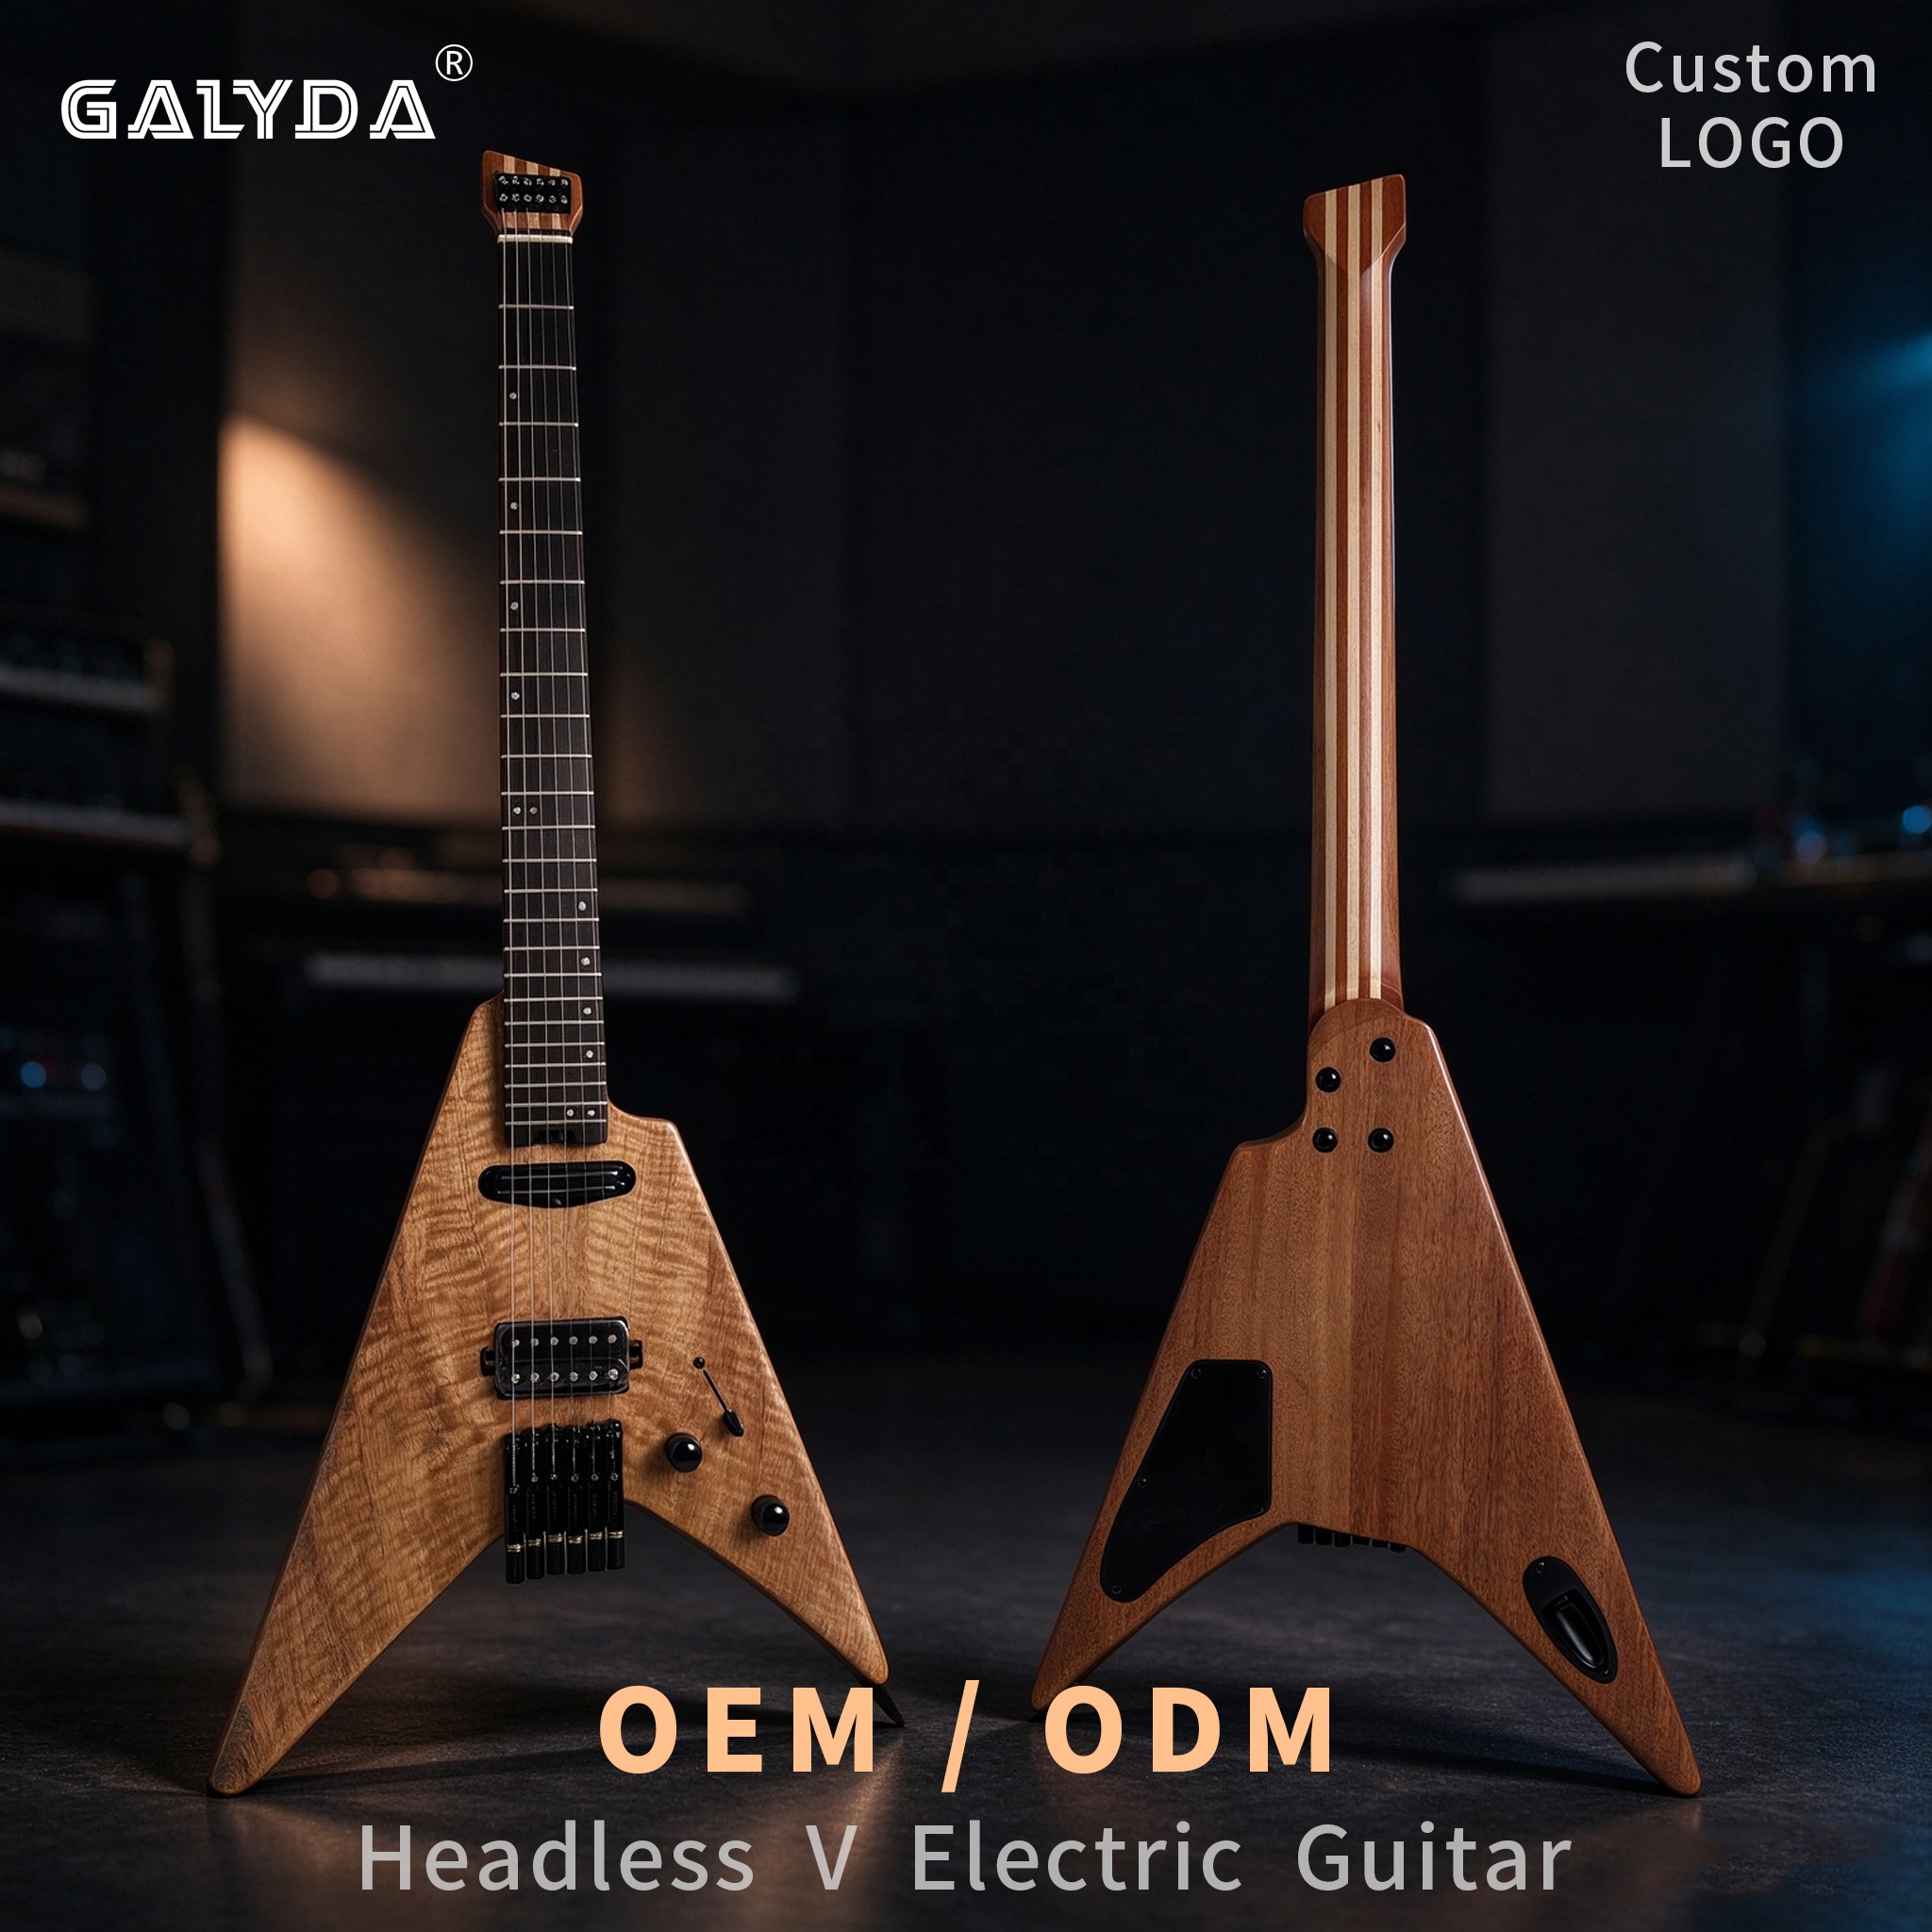
Headless V Shape Electric Guitar 6 Strings Mahogany Body 7 Piece Maple Neck Rosewood Fingerboard Guitar OEM
- Multi-ply laminate neck preventing warpage
- Selected dense rosewood fingerboard, 24 frets
- Micro-precision headless bridge locking system
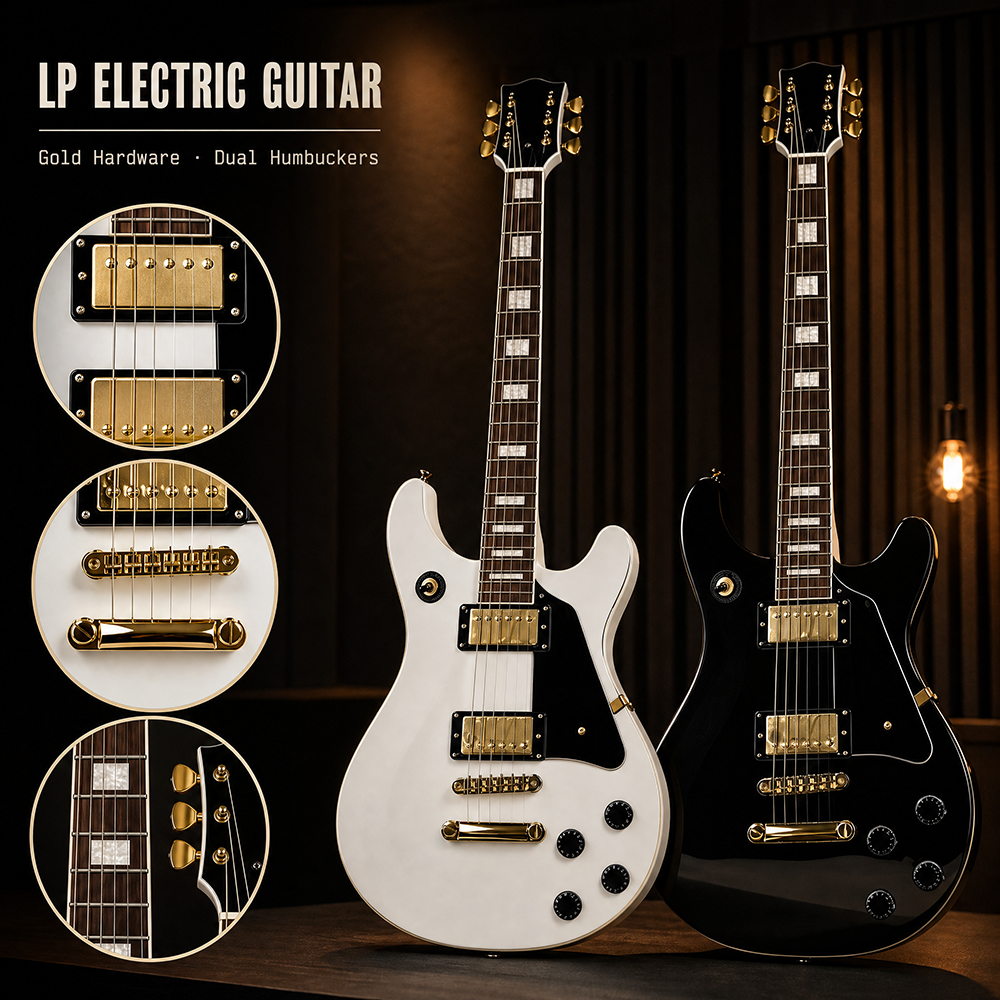
Factory Custom LP Electric Guitar Gloss Finish Solid Wood Electric Guitar OEM ODM
- Set-in neck joint with hand-leveled rosewood board
- Mirror-buffed polyurethane/nitrocellulose option
- Stable tune-o-matic bridge with bone-density nut
Engineering Structural Resilience for the Greek Microclimate
String instrument fingerboards undergo severe structural shear when transitioning between hot, arid inland Mediterranean summers and humid, saline island atmospheres. Here is how our manufacturing protocols ensure dimensional stability.
Kiln Stabilization & EMC Targeting
Standard export fingerboards dried to arbitrary moisture percentages inevitably shrink or crack when arriving at the ports of Piraeus or Thessaloniki. Our timber lots undergo automated progressive vacuum kiln-drying, locking Equilibrium Moisture Content (EMC) strictly within 6.8% – 8.2%. This prevents fret-sprout and fingerboard cupping across mainland Attica and the Cycladic archipelago.
Sub-Micron CNC Fret Slotting
Intonation failure is the primary complaint among Hellenic conservatory instructors and live acoustic musicians. Operating multi-axis heavy industrial CNC saws running diamond-coated micro-blades, NFGF cuts fret slots to a positional accuracy of ±0.012 mm. Slot depths are calibrated to tang geometries, leaving zero air pockets beneath fret crowns to guarantee continuous energy transmission.
CITES & EU Timber Regulation (EUTR)
Greek customs at maritime container depots apply rigid scrutiny to timber import permits. NFGF eliminates legal and commercial impound risk by providing complete chain-of-custody botanical documentation. Every fretboard shipment—whether harvested Rosewood, thermal Pau Ferro, or Engineered Technical Ebony—is backed by authentic non-CITES certification or verified Annex II re-export clearances.
Meeting the Demands of Greece’s Dual Classical & Folk Heritage
The Greek stringed instrument industry occupies a unique niche in Southern Europe, requiring fretboards capable of serving Western electric/classical specifications alongside endemic microtonal and traditional instruments.
The Urban Repair & Luthier Hubs of Exarcheia (Athens)
Within the historic workshop enclaves of Athens, artisan builders handle relentless refretting, custom neck resets, and bespoke classical guitar commissions. NFGF supplies semi-finished slotted fingerboards with custom radiuses (flat 0" classical, compound 9.5"-14" modern) that allow master luthiers to slash rough-prep labor hours while maintaining artisanal hand-finishing dignity.
Traditional Bouzouki, Baglamas & Laouto Hybridization
Greece’s prominent folk instrument makers require ultra-narrow, long-scale fretboards possessing high modulus of elasticity to withstand extreme metal string tension (up to 27 frets on 670mm scale lengths). Our high-density dense Indian Rosewood and black technical composites prevent longitudinal bowing under intense Greek tavern and concert rebetiko performances.
Aegean Open-Air Stage Performance Gear
Summer festival circuits across Crete, Rhodes, and Santorini expose guitars to intense heat by day and sudden maritime salt mists by night. Instrument brands manufacturing through NFGF gain access to thermal-treated (roasted) maple and resin-infused fingerboards completely impervious to salinity and atmospheric moisture swings, drastically minimizing distributor warranty claims.
Fretboard Material Behavior in Greek Climatic Conditions
A data-backed comparative reference designed to guide wholesale buyers and OEM brand specifiers in selecting appropriate fretboard substrates for Southern European export.
| Material Category | Janka Hardness Rating | Moisture Expansion Coeff. | Acoustic Tone Velocity | Greek Climate Suitability | Regulatory / EU Clearance |
|---|---|---|---|---|---|
| Selected Indian Rosewood (Dalbergia latifolia) | 2,440 lbf (10,850 N) | Medium-Low (Tangential: 5.8%) | 4,250 m/s (Warm, rich low-mid harmonic overtone) | High Stability Inland/Island | Requires CITES Appendices II Clearances |
| Thermo-Treated Pau Ferro (Machaerium scleroxylon) | 3,000 lbf (13,340 N) | Ultra-Low (Tangential: 4.1%) | 4,600 m/s (Snappy attack, percussive fundamental) | Exceptional Coastal Endurance | 100% CITES Exempt / EUTR Compliant |
| Quarter-Sawn Roasted Hard Maple | 1,450 lbf (6,450 N) | Negligible (Hydrophobic baked cell structure) | 4,850 m/s (Immediate crystalline frequency response) | Zero Fret Sprout Risk | Unrestricted Global Export |
| High-Density Technical Engineered Ebony | 3,200 lbf (14,230 N) | Zero Volumetric Movement | 4,400 m/s (Pitch-black uniform aesthetics, dry sustain) | Ideal for Budget & Academy Lines | Full CE / REACH Compliant Resins |
| Standard Non-Treated Laurel Wood | 1,820 lbf (8,100 N) | High (Tangential: 7.9%) | 3,950 m/s (Muffled low register if moisture exceeds 12%) | Requires Controlled Case Storage | Non-CITES Generic Standard |
Huizhou NFGF: Industrial Scale Built on Luthier Precision
Operating from our modern 5,100 m² instrument manufacturing complex in Qiuchang, Huizhou, we combine cutting-edge automated machining with authentic luthier assembly lines.
SGS On-Site Audited Assurance
Our facility was independently examined by the world-leading SGS Group (audit valid November 2025). We maintain verified controls over incoming raw wood conditioning, adhesive tensile strength, electronic soldering, and pre-dispatch action inspection.
Low MOQ & Private Label Agility
Unlike massive conglomerates demanding full-container commitments per SKU, NFGF supports agile European business models. OEM electric guitars and sample neck batches start from low MOQs, allowing boutique Greek brands to test models without working capital strain.
Full Chain Quality Protocols
Each fingerboard blank undergoes four critical control gates: acoustic tap testing for interior micro-checks, electronic moisture verification, CNC precision verification via optical gauges, and final hand-burnishing of edge bevels for immediate playability.
Greek Importers & Luthiers: Frequently Asked Questions
Clear, direct answers regarding logistical execution, European tax conformity, customs clearance, and specification parameters.
Q: What documentation is provided for Greek Customs import clearance at Piraeus port?
We supply commercial invoices formatted with exact HS codes (e.g., 9209.92 for instrument parts/fretboards, 9202.90 for completed guitars), detailed packing lists with net/gross weights, Certificate of Origin, and relevant CITES export verification or phytosanitary declarations to prevent Hellenic Customs delays.
Q: How do your fretboards endure shipping through the Suez Canal and Aegean humidity spikes?
All finished fretboards and neck blanks are sealed with moisture-impervious shrink film containing food-grade desiccant packets, packed in heavy-duty export carton outers. This eliminates exposure to saline sea fog and catastrophic relative humidity fluctuations during transit.
Q: Can you mill custom scale lengths and fret counts for traditional Greek instruments?
Yes. Our in-house CAD/CAM engineers can program non-standard scales including 650mm, 670mm, or multi-scale fan fret designs, with customized fret-wire tang widths (0.5mm – 0.6mm) tailored to your preferred nickel-silver or stainless steel fret wire.
Q: What are the standard lead times for OEM fretboard runs delivered to Greece?
Sample fretboard batches typically complete CNC profiling and hand-finishing within 10 to 15 working days. Production runs of 200–1,000 units are manufactured in 30–35 days, followed by direct maritime freight (approx. 22–28 days to Piraeus) or air freight express for urgent workshop repairs.
Q: Can we request unslotted, radius-only, or completely pre-fretted finished boards?
We offer complete modularity: raw kiln-dried blanks, slotted flat boards, compound radiused boards with pearl/abalone/glow dot inlay installations, or fully pre-fretted and edge-dressed fingerboards ready to glue directly to your neck billets.
Q: How does NFGF assist Greek businesses with EU VAT and EORI formalities?
We work seamlessly with your nominated Hellenic customs broker or can arrange door-to-door DDP (Delivered Duty Paid) shipments for smaller consignments, ensuring your Greek EORI number and intra-EU VAT accounts are accurately credited without processing friction.
Accelerate Your Instrument Manufacturing & Parts Sourcing
Whether you require kiln-stabilized tonewood fingerboards for a boutique Athenian workshop or custom-branded electric and acoustic guitars for national distribution in Greece, our engineering team is ready to review your CAD files and technical specifications.